What Are the Main Industrial Coating Methods?
 October 28, 2026
 Hits:9second
What Are the Main Industrial Coating Methods?
Coating methods may be named for how material is applied, how it is deposited, or the film a process is designed to form. Spraying, roll coating, curtain coating, flow coating, and dipping are common application methods. Powder coating and electrodeposition involve different deposition processes, while spin, slot-die, and meniscus coating serve more specialized film requirements. Suitable options depend on the part, coating material, required finish, and production conditions.
Main Industrial Coating Methods
Spray Coating
Spray coating atomizes liquid coating material and directs it onto a part. Air spray uses compressed air to break liquid into droplets. Airless spray relies on fluid pressure. Suitable systems may also use electrostatic assistance.
A spray gun does not need to touch the part, making spray coating useful for shaped surfaces, edges, and multiple faces. Coverage still depends on access. Recesses, corners, or surfaces facing away from the gun may need another spray angle or pass. Areas that must remain uncoated may require masking.
Coating that misses the part becomes overspray, increasing material loss and work in the spray area. Gun distance, angle, and overlap between passes also affect coating uniformity.
In a spray process, production lines may use reciprocating machines, five-axis systems, or robots to move spray guns along programmed paths. Such equipment can repeat movements across similar parts or approach surfaces from different angles. Gun paths and settings still need to suit part geometry and finish requirements.

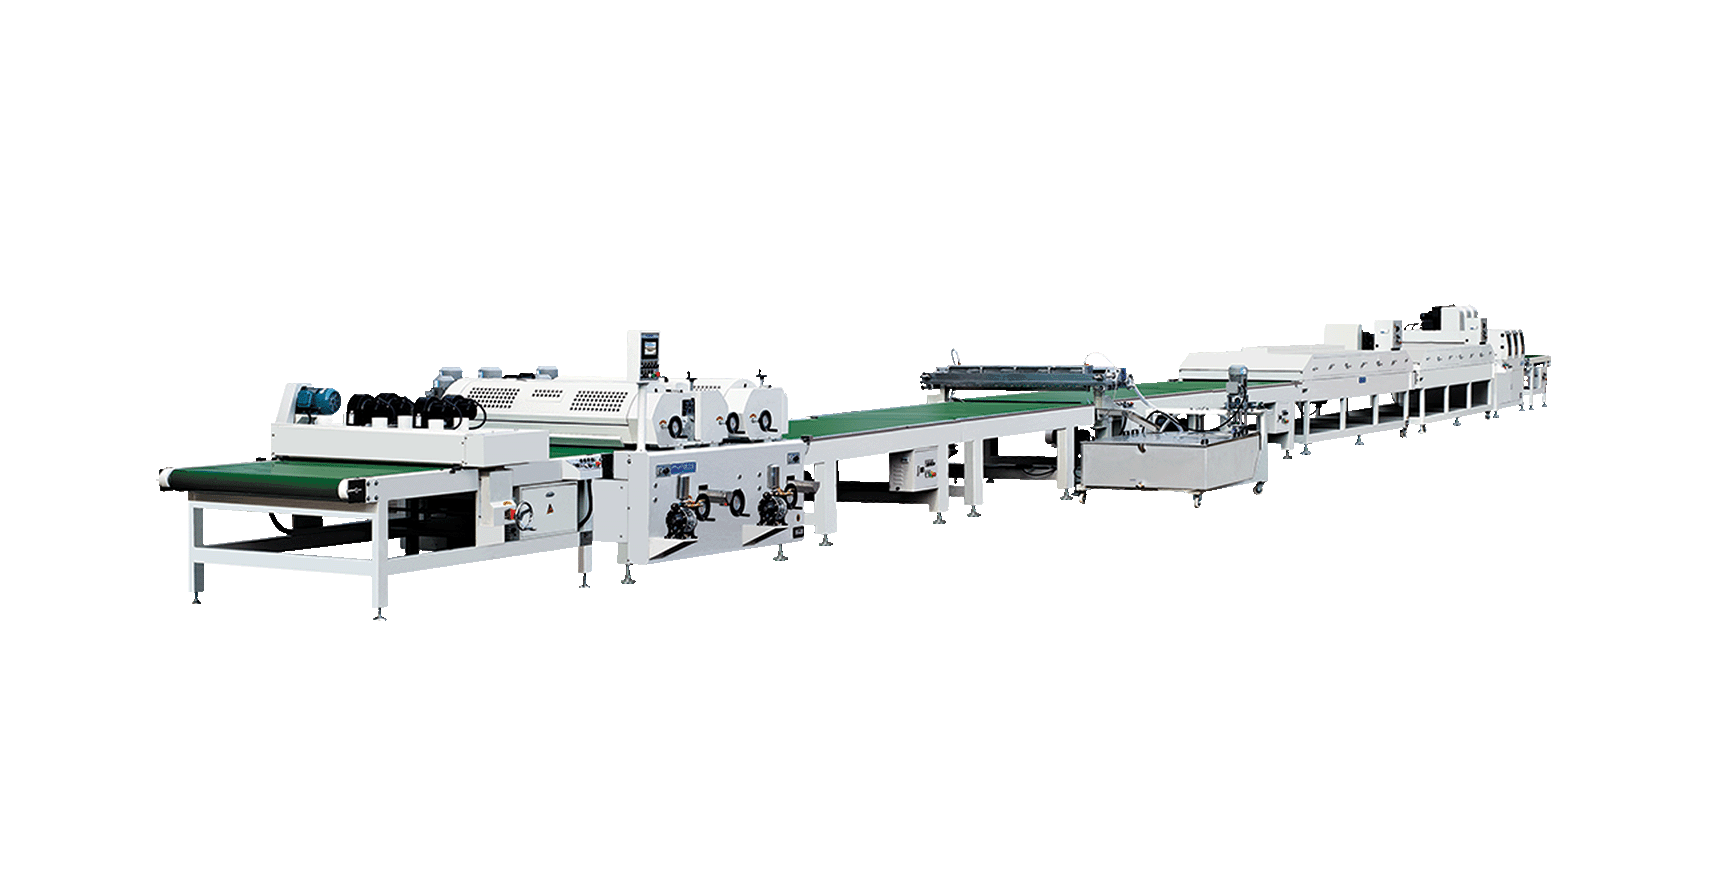
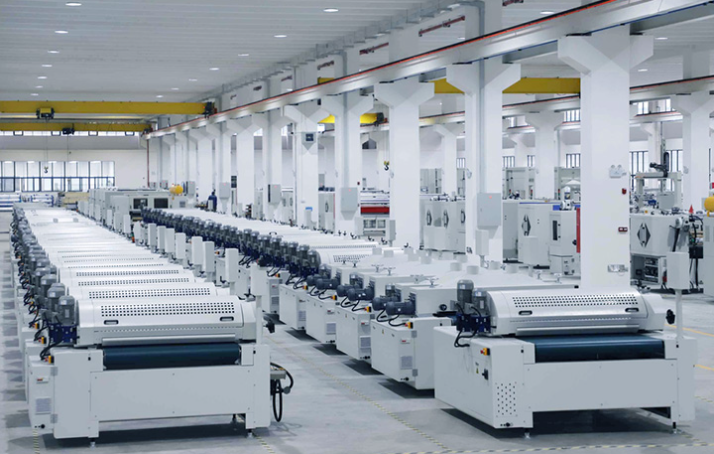
PURETE spray coating production line
Roll Coating
Roll coating transfers coating material to a part through rotating rollers. Panels move past coating rollers for continuous application. Flat boards and door panels are common candidates because their surfaces can maintain contact with a roller.
Coating supply, metering, roller configuration, and running conditions all affect the result. Metering influences how much material transfers to a panel. Roller speed, contact pressure, and surface condition can change how evenly coating is applied. Worn or contaminated rollers may leave visible differences in the finish.
Direct contact also limits suitable part shapes. Recesses, raised details, and pronounced contours may receive uneven coverage or remain uncoated. Surface profile therefore matters as much as substrate material when assessing a part.
Curtain Coating
Curtain coating creates a continuous falling sheet of liquid from a coating head. A conveyor carries panels through this liquid curtain, allowing coating to reach their upper surfaces. Flat boards and door panels are typical candidates when they can move steadily through the coating area.
No roller contacts the coated surface during application. Curtain coating can be considered for smooth finishes, including high gloss, but suitability depends on coating material, part shape, and required appearance.
Coating supply, head opening, and conveyor movement must support a stable curtain. Bubbles or breaks in the liquid sheet can interrupt coverage and leave visible defects. Part shape and transport through the curtain also need to be assessed.
Flow Coating
Flow coating directs liquid coating onto a part and lets it run across the surface. Excess liquid drains away. Unlike curtain coating, liquid moves over the part rather than forming a falling sheet that the part passes through.
Part position determines where coating flows, which surfaces it reaches, and where excess material collects. Shape changes can interrupt flow. Recesses and low points may retain liquid, causing buildup or an uneven finish. Both coverage and drainage need to be checked against the coating material and desired result.
Dip Coating
Dip coating immerses a part in a liquid coating bath. After withdrawal, excess coating drains from the part. Immersion can bring liquid to several surfaces, including some areas that are difficult to reach with a spray gun or roller.
Part size must suit the bath, and positioning must allow liquid to reach intended surfaces. Air trapped in a blind hole or cavity can prevent coverage. Those same features may retain excess coating after withdrawal, leaving buildup or an uneven finish.
Bath size, part handling, withdrawal, and drainage all affect whether immersion is practical. Complex geometry alone does not make a part suitable for dip coating. Liquid needs a route in and, where necessary, a route out.
Brush and Roller Application
Brushes and handheld rollers apply coating through direct contact. Industrial uses include on-site coating, repairs, touch-ups, and parts or areas that are impractical to coat on a production line. Brushes can reach edges and details. Handheld rollers can cover accessible, relatively flat surfaces.
Manual application requires more time and labor as an area grows or becomes harder to reach. Appearance may also vary with application technique.
Powder Coating and Electrodeposition Processes
Powder Coating
Powder coating applies dry coating material to a part. Electrostatic spraying is a common approach: charged powder is directed toward a part and deposited on its surface. Curing then forms a continuous coating. Powder coating can therefore use spraying, although the material differs from liquid coating used in the spray process described earlier.
Many metal parts can be powder coated. Suitable nonmetallic substrates are also possible. Application and curing conditions must fit the substrate. During electrostatic spraying, recesses and inside corners can be harder to cover evenly than exposed surfaces.
Part size, required finish, curing equipment, and production schedule influence the choice. Frequent color changes may add cleaning and changeover work. Evaluation should include both powder application and curing.
Electrodeposition Coating (E-Coating)
E-coating immerses a conductive part in a liquid coating bath. An electric field between the part and electrodes in the bath drives coating material onto the part’s surface. Ordinary dip coating also involves immersion, but does not use electrically driven deposition.
A bath may reach some areas that are difficult to spray. Coverage still depends on part geometry and whether liquid can enter those areas. E-coating deposits coating material; electroplating deposits metal.
E-coating requires a conductive surface, a coating bath, electrical equipment, and steps such as rinsing and curing. Part size, bath access, coating requirements, and integration with other production stages all affect suitability.
Specialized Methods for Precision Coating
Some applications need close control over film formation on a wafer, sheet, or other substrate. Spin coating, slot-die coating, and meniscus coating form films through different ways of supplying and spreading liquid.
Spin coating spreads liquid across a rotating substrate. Rotation distributes liquid and removes excess material, leaving a thin film. Flat substrates such as wafers are common candidates. Size, shape, liquid properties, and film requirements determine suitability. Large or strongly contoured parts can be difficult to process this way.
Slot-die coating feeds liquid through a narrow die opening onto a moving substrate. Continuous processing can use this method to control coating width and liquid supply. Flow rate, die-to-substrate gap, substrate speed, and liquid properties must be matched to maintain stable coating.
Meniscus coating maintains a small bridge of liquid between a supply surface and a substrate. Relative movement draws liquid into a film. This term covers several equipment arrangements and can overlap with slot-die coating. Equipment setup, liquid properties, substrate, and film requirements determine suitability.
How to Choose the Right Industrial Coating Method
Part geometry, coating requirements, and production conditions shape the choice. The table summarizes typical uses, benefits, and constraints before the four checks below.
| Method or Process | Typical Parts or Applications | Main Advantages | Main Limitations |
|---|---|---|---|
| Spray coating | Shaped furniture parts and multi-sided components | Gun position can be changed to coat different faces and edges | Overspray adds material loss and cleanup; recesses may need extra passes |
| Roll coating | Flat boards and door panels | Coats flat surfaces continuously as panels move through the equipment | Raised details and recesses interrupt roller contact |
| Curtain coating | Flat boards and door panels | Applies a continuous coating without roller contact on the coated surface | Unsteady transport or breaks in the curtain can leave defects |
| Flow coating | Parts with open surfaces and a drainage path | Liquid can run over shaped surfaces without direct tool contact | Low points and recesses may retain excess coating |
| Dip coating | Parts that fit in a coating bath | Immersion brings liquid to several accessible surfaces | Blind holes and cavities may trap air or coating |
| Brush and handheld roller application | On-site work, repairs, and touch-ups | Treats local areas without moving work to a coating line | Large areas require more labor; appearance may vary |
| Powder coating | Metal components and housings suited to curing | Suitable systems can collect and reuse powder that misses a part | Curing conditions limit suitable parts; recesses can be difficult to coat by electrostatic spray |
| E-coating | Conductive metal components and vehicle bodies | Bath deposition can reach some areas that are difficult to spray | Requires conductivity, bath access, and suitable production equipment |
| Spin coating | Wafers and other flat, rotatable substrates | Spreads liquid into a thin film on a rotating surface | Large or irregular substrates can be difficult to mount and coat |
| Slot-die coating | Moving films, foils, and other webs | Meters liquid supply during continuous coating | Flow rate, speed, and die gap must be matched |
| Meniscus coating | Flat sheets or other substrates in meniscus-guided setups | A maintained liquid bridge helps control film formation | Changes in liquid flow or movement can destabilize the meniscus |
Step 1: Check the Substrate and Part Geometry
Start with substrate material. E-coating, for example, requires an electrically conductive surface. Then consider part size and shape. Flat panels may suit roll or curtain coating. Shaped parts need closer checks of edges, recesses, and surfaces facing different directions.
Immersion and flow processes also require attention to trapped air and retained coating. Confirm that each part fits the equipment and can be held or conveyed without blocking surfaces that need coating.
Step 2: Define the Coating and Finish Requirements
Identify the coating’s role, such as primer or topcoat, and the desired appearance, such as high gloss or matte. Check required coverage and film uniformity, then confirm that each candidate method suits the coating material. Different methods may produce a high-gloss or matte finish, depending on the material, substrate, and process setup.
Mark any areas that must remain uncoated. Selective application or masking may be needed. The proposed process must meet both coating requirements and appearance requirements on the actual substrate.
Step 3: Check Drying and Curing Requirements
Coating application is only one stage of film formation. Drying or curing conditions must suit both coating material and part. Size and shape also determine whether the part can pass through the required equipment.
A method may apply coating successfully but remain impractical if suitable drying or curing cannot follow.
Step 4: Assess Production Needs and Total Cost
Production volume, required pace, color changes, and part changes affect process choice. Equipment must work with part handling, conveying, and other production stages. Automation can repeat planned movements or settings, but its value depends on the product mix and production requirements.
Compare cost per finished part under expected conditions. Include equipment, labor, coating material, energy, cleaning, maintenance, and rework.
Conclusion
Industrial coating methods offer different ways to reach a surface and form a film, from spraying and roller contact to immersion, powder application, and electrically driven deposition. Suitable choices depend on part shape, coating requirements, and production conditions. Equipment information and trials with actual parts can help confirm a choice. Surface preparation and process control also affect the finished coating.
Exploring coating equipment for your production line? Contact PURETE to discuss your project requirements.
Frequently Asked Questions
Can powder coating be applied by spraying?
Yes. Electrostatic spraying is a common way to apply powder coating. Spraying describes how coating is applied; powder coating refers to the material and process. Liquid coatings can also be sprayed.
Are curtain coating and flow coating the same?
No. Curtain coating passes a part through a falling sheet of liquid. Flow coating directs liquid across a part’s surface, then drains away excess material.
What Is the Principle of Auto Coating Machine?

Advantages of Short-Cycle Presses in Panel Processing
Application of Soft-Touch (Excimer) Coating in Furniture and Decorative Materials
Which Industries Benefit Most from PUR Laminating?
What Is the Principle of Roller Coating Machine?
How Does PUR Laminating Compare to Solvent-Based Lamination in Terms of Cost?
Global Surface Finishing Market Analysis and Development Trends


